

Different zero-setting methods are available according to the characteristics of the project to be carried out (profile type and blade inclination).
Profile along X and machining with the blade vertical
A axis: 0_; C axis: 0_
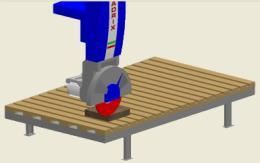
Axis | Origin zero setting | Visual reference |
X | Spindle centre aligned with the start of the profile. | 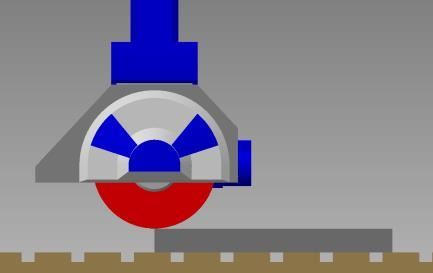 |
Y | Outer edge of the blade aligned with the end of the section (usually corresponding to the lower horizontal side of the unmachined workpiece). | 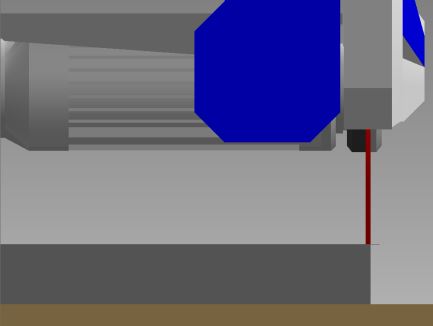 |
Z | Blade just touching the material surface. | 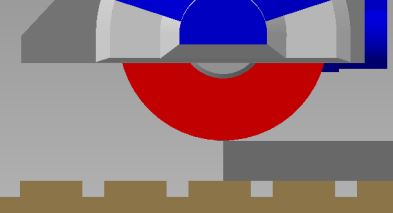 |
Profile along Y and machining with the blade vertical
A axis: 0_; C axis: 90_
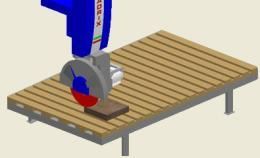
Axis | Origin zero setting | Visual reference |
X | Outer edge of the blade aligned with the end of the section (corresponding to the left side of the unmachined workpiece when machining the left-hand part of the workpiece). | 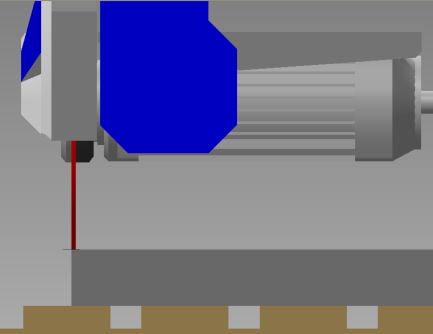 |
Y | Spindle centre aligned with the start of the profile. | 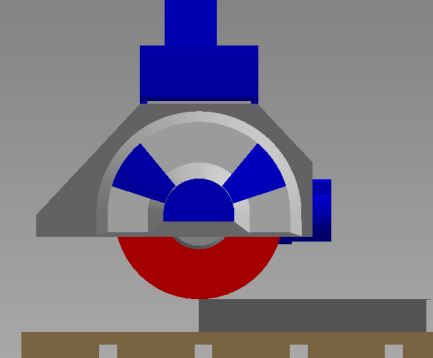 |
Z | Blade just touching the material surface. | 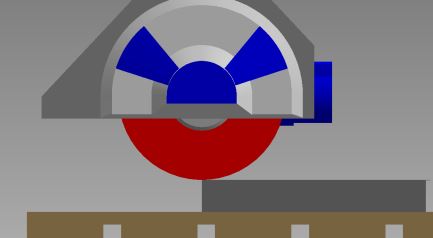 |
Profile with a segment along X and machining with the blade horizontal
A axis: 90_; C axis: 0_
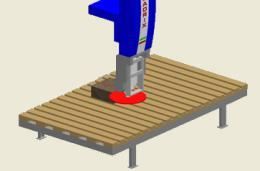
Axis | Origin zero setting | Visual reference |
X | Spindle centre aligned with the start of the profile. | 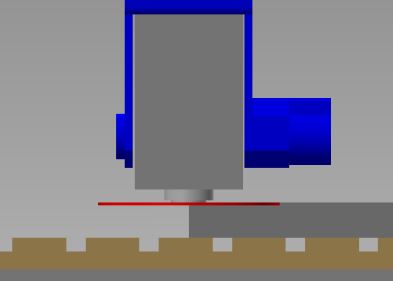 |
Y | Blade just touching the lower horizontal side of the unmachined workpiece (end of the section). | 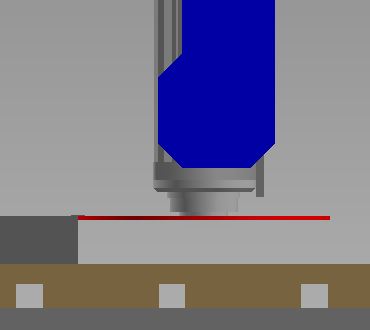 |
Z | Inner edge of the blade level with the material surface. | 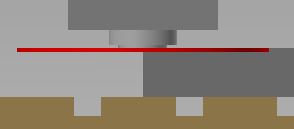 |
Profile along Y and machining with the blade horizontal
A axis: 90_; C axis: 90_
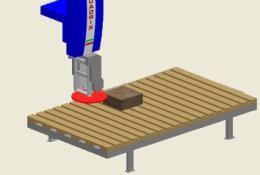
Axis | Origin zero setting | Visual reference |
X | Blade just touching the left side of the unmachined workpiece (corresponding to the left side of the unmachined workpiece). | 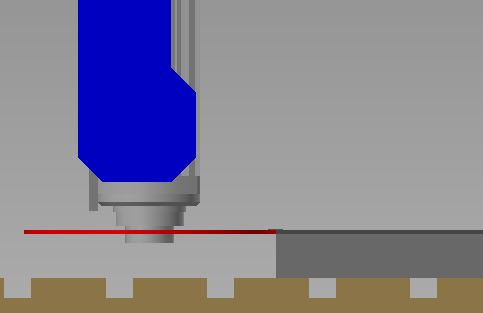 |
Y | Spindle centre aligned with the start of the profile (corresponding to the upper horizontal side of the unmachined workpiece). | 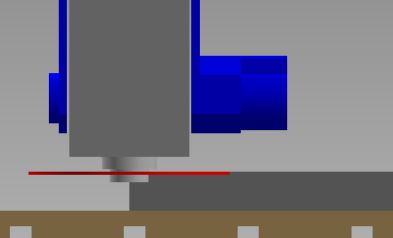 |
Z | Inner edge of the blade level with the material surface. | 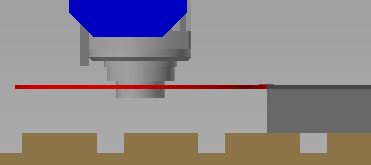 |
