

IsoCam is software for carrying out profile machining with the disk; it can be used to draw or import shapes, define the profile and apply different machining methods.
Working programming is divided into several stages, which are described in the following paragraphs.
When the IsoCam program is opened, if no working has previously been created, the operator can create a new one starting from the first working step.
If a working has previously been created, it is loaded automatically and the operator is taken directly to the last step of the working:
Elements common to the various steps
The user interface consists of several areas.
Menu: quick utilities.
Top bar: functions specific to the active page.
Central area: contains the drawing or active area depending on the page.
Sidebar: window containing the parameters to be edited.
Bottom bar: buttons generally available in several areas of the software.
The following elements remain visible at all times, regardless of the current stage of the process.
Menu
The menu bar is located at the top, above all other elements of this interface.
Visible | The operator is provided with several settings relating to the visibility of the pieces in the work area. |
Options | Colour-related settings can be changed. |
Language | ISOCAM is currently available in the following languages:
|
Right sidebar
 | Machine settings |
 | Info |
 | Step Management |
 | Close |
Machine settings
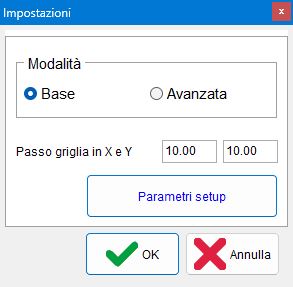
This panel allows you to switch to IsoCam Advanced mode, return to the basic version, and edit the Grid Step values in X and Y.
Bottom bar
 | New working |
 | Working files |
 | Save working |
 | Edit Working |
Section drawing (step 1 of 4)
The first programming stage consists of drawing the section to be machined. The window provides the typical commands of CAD software: draw line, draw arc, snap, move, etc.
The software is based on creating the section as a quick sketch that is then edited entity by entity using the dedicated commands. Drawings in .dxf format generated by external CAD systems can still be imported at any time.
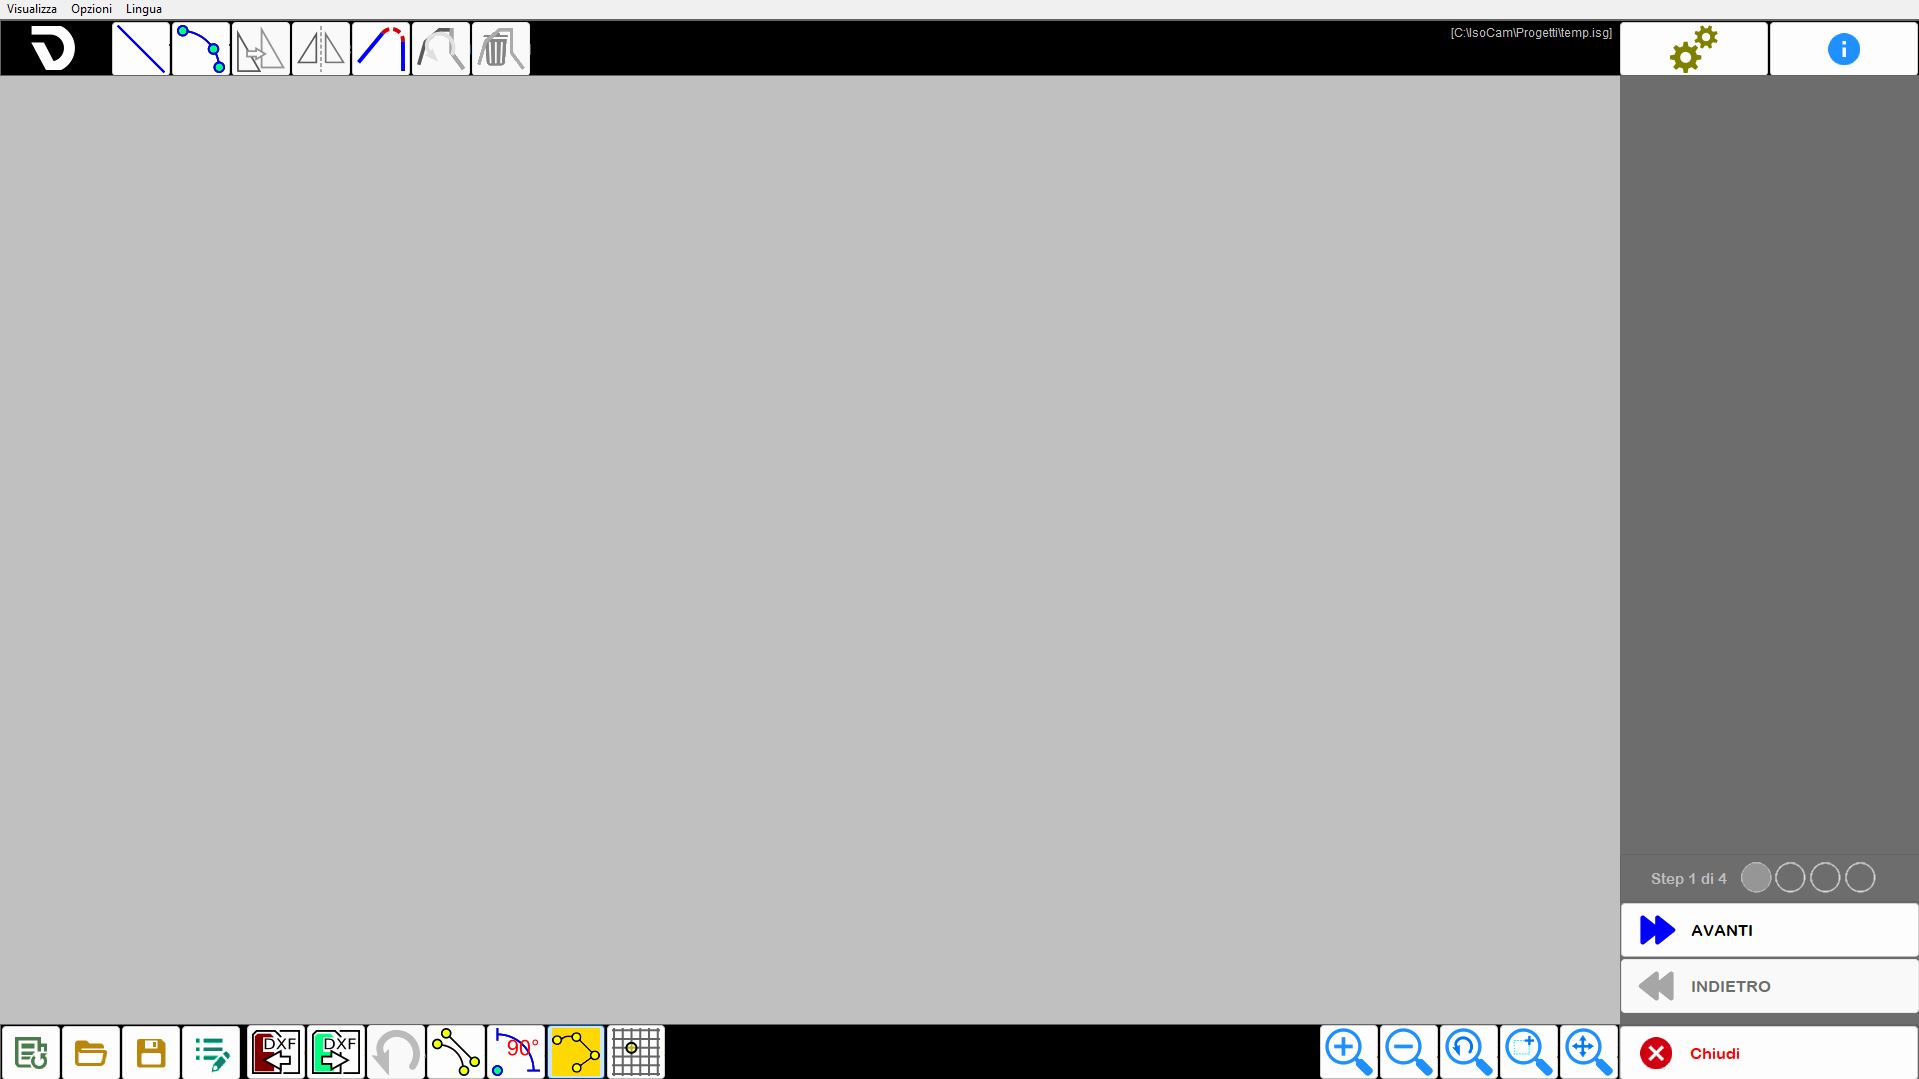
Top bar
 | Line drawing command |
 | Arc drawing command |
 | Move selected segments |
 | Mirror Figure |
 | Fillet |
 | Invert active selection |
 | Delete selected segments |
Right sidebar
Line properties
When a line is selected in the work area, the right sidebar is updated to show the characteristics of the selected entity, which can be edited by the user:
Length | Indicates the linear distance between the two endpoints of the selected line, calculated from their coordinates in the work space. |
Angle | Indicates the orientation of the line relative to the horizontal axis of the reference system. |
Δx | Indicates the change in the X coordinate between the start and end points of a line or entity, i.e. the horizontal distance travelled relative to the X axis of the reference system. |
Δy | Indicates the change in the Y coordinate between the start and end points of a line or entity, i.e. the vertical distance travelled relative to the Y axis of the reference system. |
 | Extend/Shorten selected line |
 | Approximate Angle |
Scale connected segments | Allows proportional scaling to be applied to all entities directly or indirectly connected to the selected line. |
Arc properties
When an arc is selected in the work area, the right sidebar is updated to show the characteristics of the selected entity, which can be edited by the user.
The arc can be defined in different ways: by points, as centre, radius and arc, etc.
The various characteristics are shown in the window that appears on the right.
A change to certain characteristics can be achieved in different ways, for example by changing the radius or the start/end point; the “Fixed centre” flag determines how the change is applied.
Radius | Indicates the constant distance between the centre of a circular curve or arc and any point along its circumference. |
Start/end angle | Angle of the start or end point relative to the centre. |
Prev. / Next Tangent | Changes the start or end angle so that the arc is tangent to the previous or next entity. |
Fixed centre | Determines the consequences of a change (radius or angle). |
Translate / Move selection
When the “move” command is enabled, the window containing the movement parameters appears. Movement can be performed directly by clicking in the drawing area (including with snaps active) or by setting the parameters.
The movement must be confirmed using the “OK” button.
 | Position selector |
 | Translation |
Move copy | When enabled, the function creates a copy of the selected entity and applies the movement only to this copy, leaving the original entity unchanged. |
Mirror
After enabling the command, set the centre of symmetry by clicking in the work area or entering the positions, select the mirror direction and press the “OK” button to confirm.
Centre of symmetry | Allows the coordinates of the centre of symmetry used to flip the selected entity horizontally or vertically to be changed. |
Coordinates to invert | Indicates whether to flip horizontally, vertically or in both directions. |
Mirror copy | When enabled, the mirroring operation is performed by creating a mirrored copy of the selected entity while leaving the original unchanged. |
Fillet
A first message displayed in the right column allows the operator to set the fillet radius and confirm the selection.
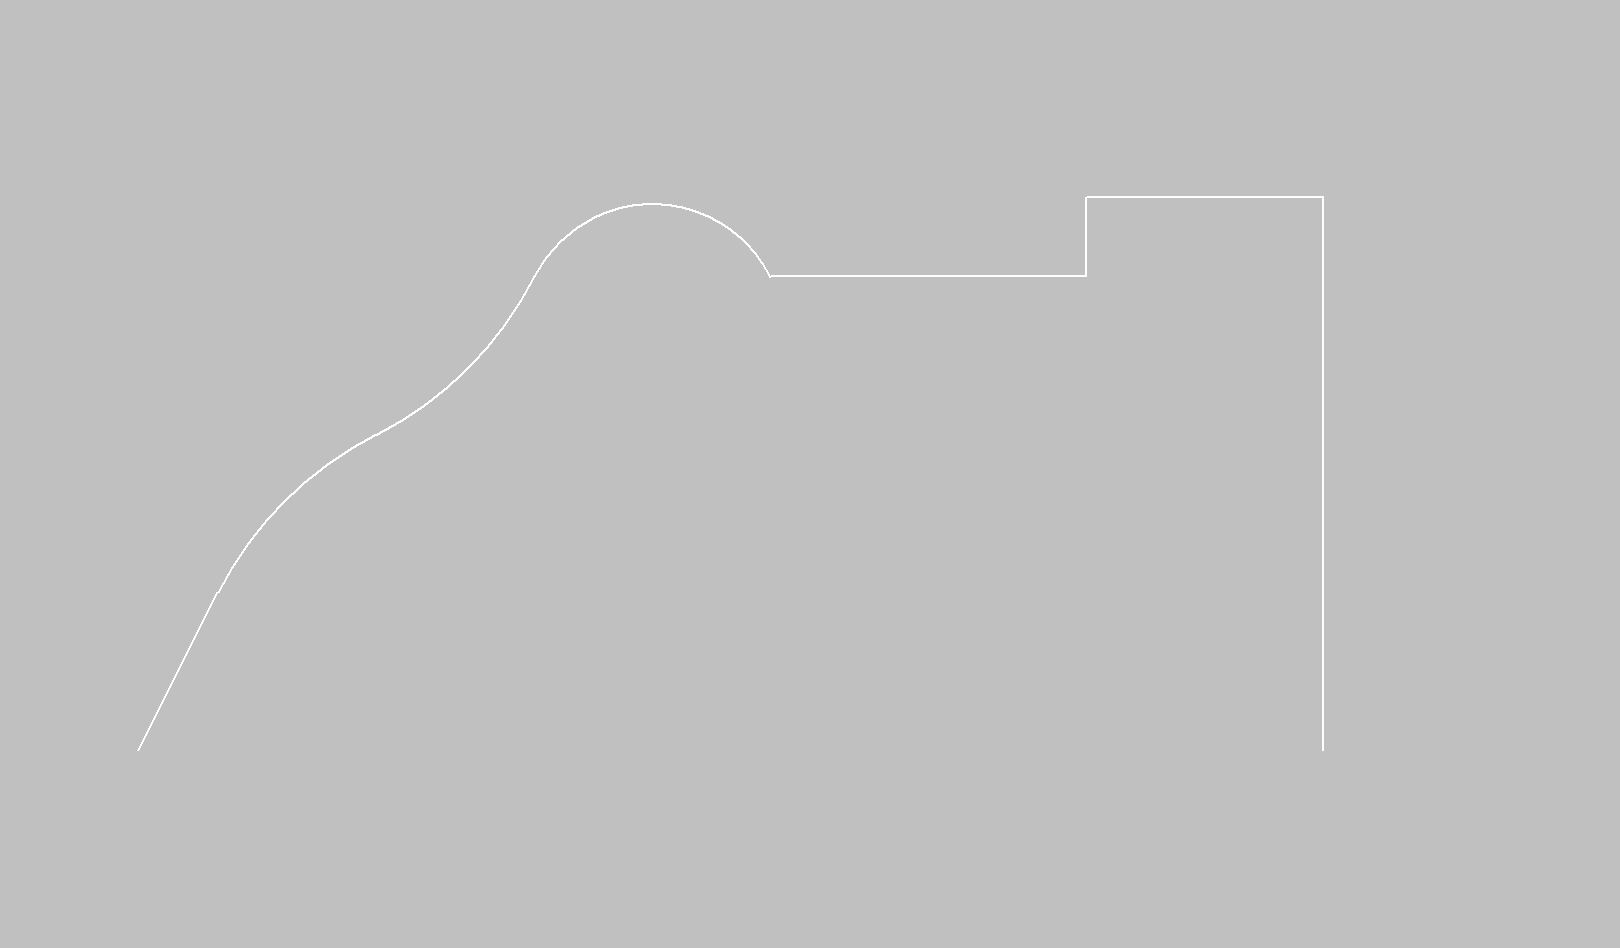
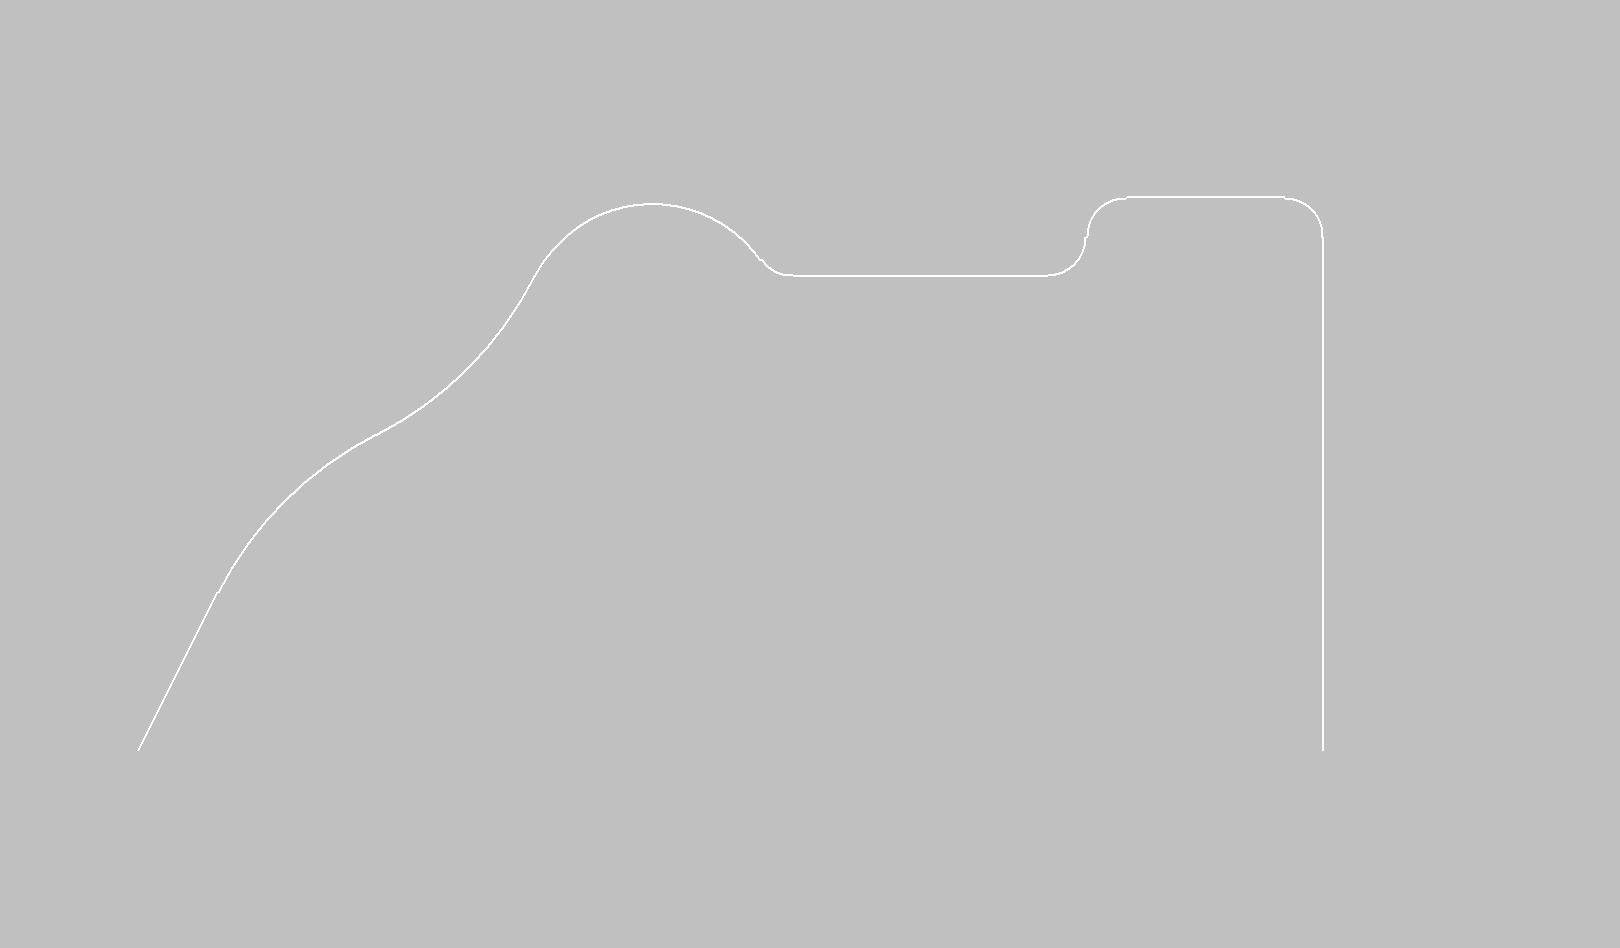
A second message informs the operator that fillets can now be inserted between two lines; this remains available until the function is disabled.
The following example shows fillets applied to two adjacent lines and to a line adjacent to an arc:
After applying the fillets:
Bottom bar
 | Import DXF file |
 | Export DXF file |
 | Undo change |
 | Start/end snap |
 | Ortho command |
 | Connected Segments command |
 | Drawing grid |
 | Undo Zoom |
 | Select area for Zoom |
 | Reset Zoom |
Profile selection (step 2 of 4)
The previously drawn section must be applied to a suitable profile.
The profile can be linear or arc-shaped, in the X/Y plane or vertical; depending on the selection, certain working modes are enabled or disabled. For example, an arc profile in the XY plane can only be machined with the disk vertical, and vice versa for an arc profile in the XZ or YZ plane.
The profile type is selected using the buttons on the left; the parameters used to describe the profile geometrically are shown at the top centre, and a preview of the result is shown in the lower central area.
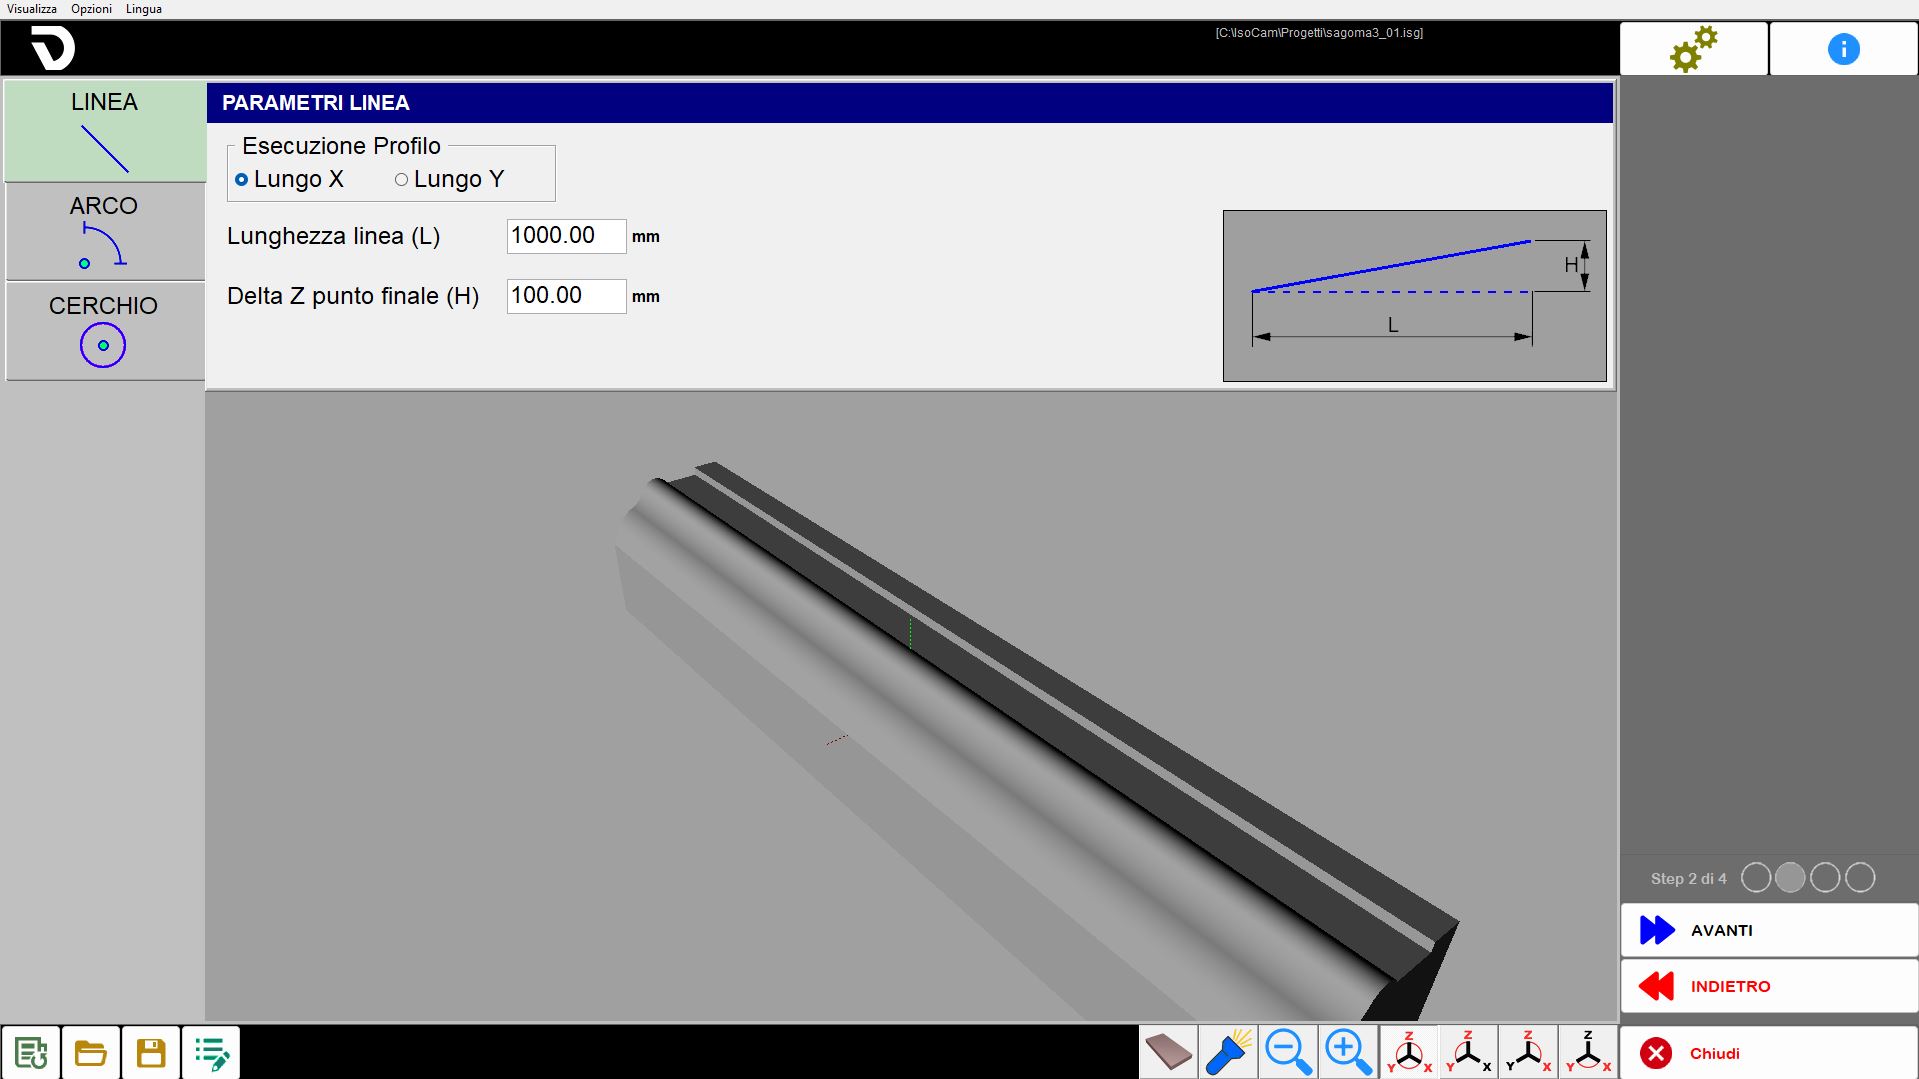
Central area
Linear Profile | Set the direction and length. |
Arc Profile | Define the direction, working plane, concavity and geometric characteristics. |
Circular profile | It is machined externally only, with the disk horizontal. |
Linear Profile parameters
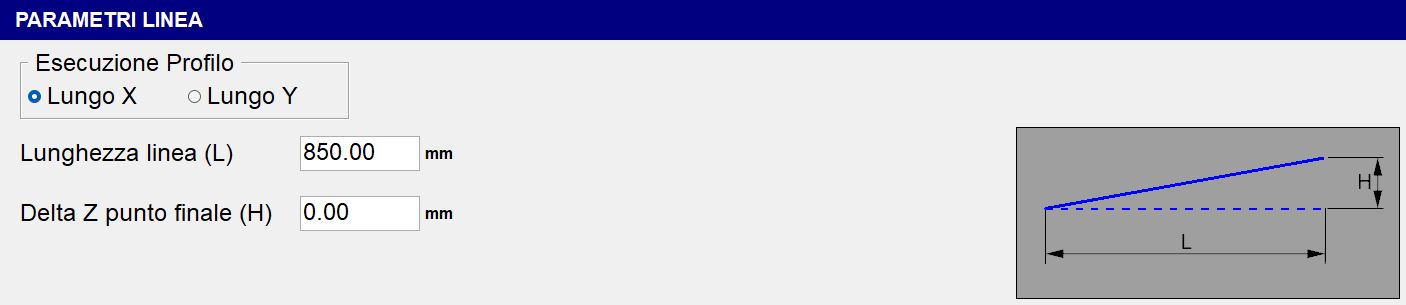
Profile Execution | Two modes are available: “Along X” and “Along Y”. |
Line length (L) | Horizontal length of the base of the inclined segment, measured between the starting point and the horizontally projected end point. |
End point Delta Z (H) | Height of the inclined segment, i.e. the difference in position between the start and end of the segment. |
Arc Profile parameters
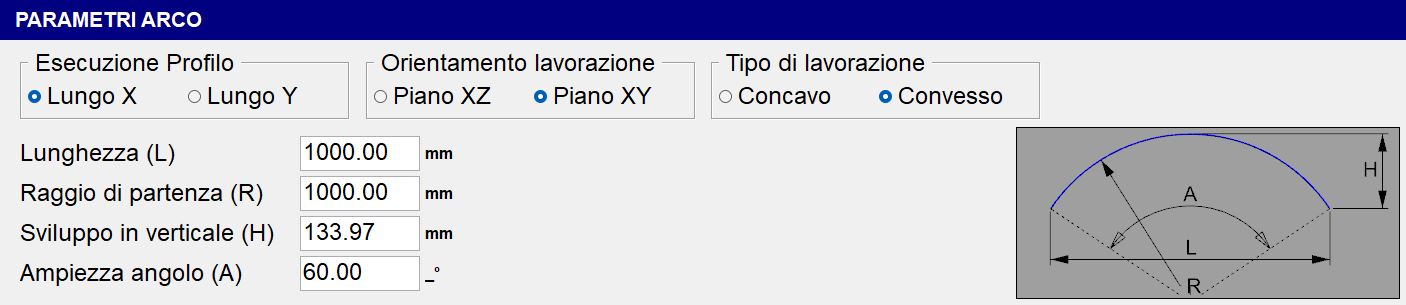
Profile Execution | Choice between “Along X” or “Along Y”. |
Working orientation | Choice between “XZ Plane” or “XY Plane”. |
Working type | Choice between “Concave” or “Convex”. |
Length (L) | Horizontal distance between the two endpoints of the arc, i.e. the chord connecting the start and end of the arc. |
Starting radius (R) | Distance from the centre of the arc to a point on the arc itself. Determines the overall curvature of the arc. |
Vertical development (H) | Maximum height of the arc relative to chord L; represents the vertical distance between the highest point of the arc and the chord. |
Angle amplitude (A) | Central angle subtended by the arc, expressed in degrees. |
Changing any of the following values: “Length”, “Starting radius”, “Vertical development” or “Angle amplitude” automatically recalculates the remaining parameters.
Circular Profile parameters
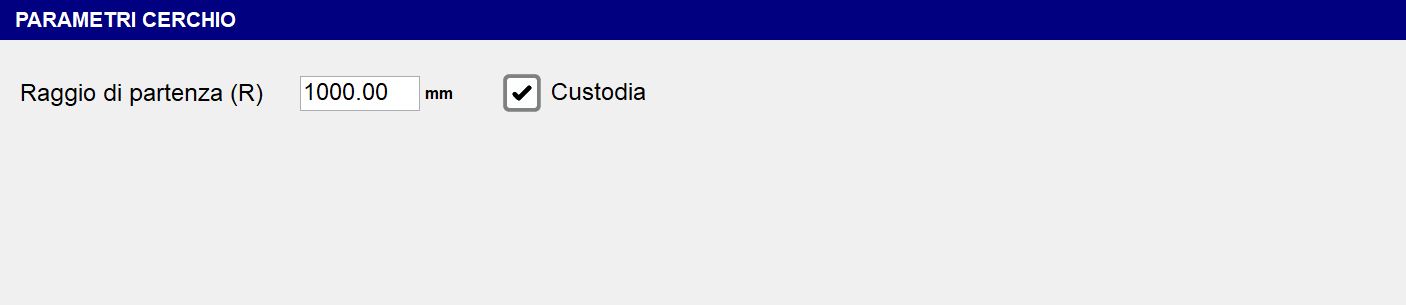
Starting radius (R) | Determines the radius from the starting point. |
Guard | This flag indicates whether the C axis rotates during the working phase (guard active) or remains stationary with C=0_ (guard not present). |
Bottom bar
 | Worktable view |
 | Additional lights |
 | Default view management |
Working parameters (step 3 of 4)
The page is divided into panels containing different types of data to be set for the working.
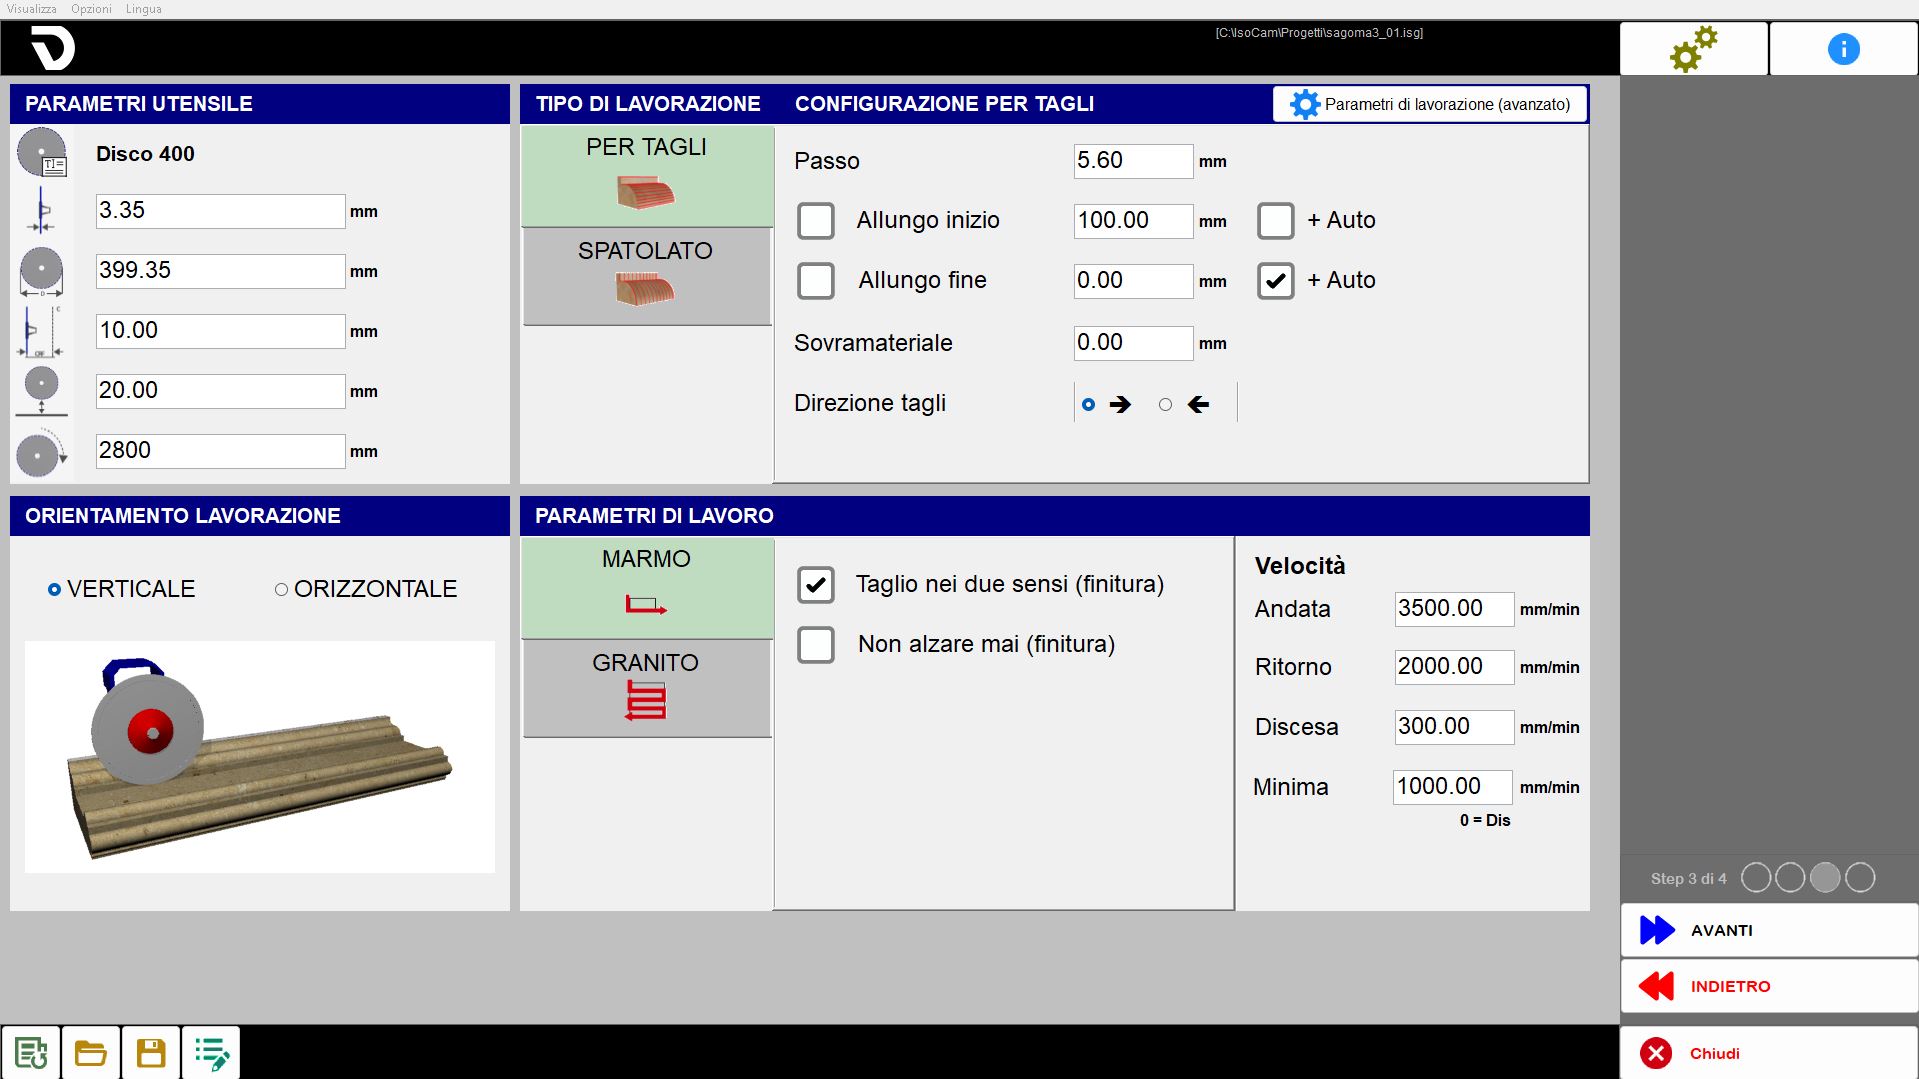
Parameters tool
The operator can define the tool parameters:
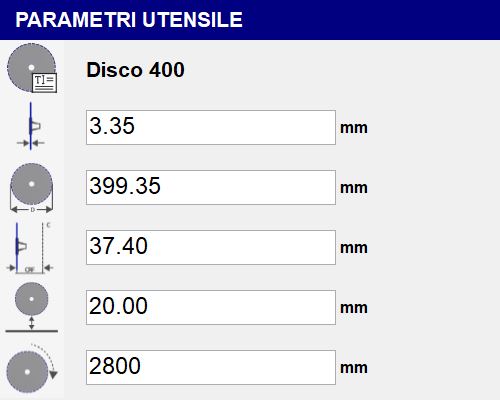
For a new project, the data is loaded automatically based on the tool physically installed; for a previously saved working, the tool data is the data already saved in the previous program.
 | Tool name |
 | Thickness |
 | Diameter |
 | CRF (Flange Rotation Centre) |
 | Safety position |
 | RPM (Revolutions Per Minute) |
Working orientation
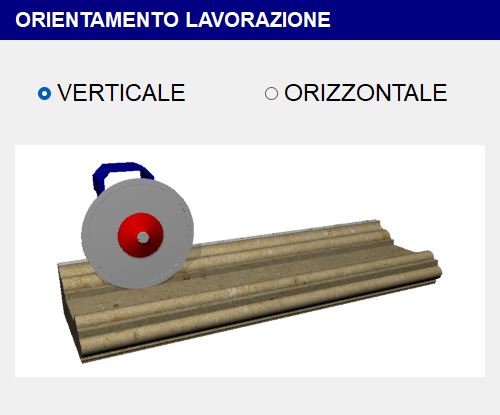
Linear Profile
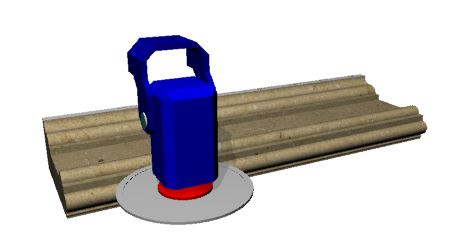
For linear profiles, it is possible to choose whether to perform the working with the disk vertical or horizontal (from the front or from the left).
Vertical Orientation | Horizontal Orientation |
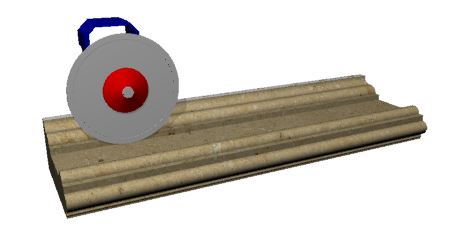 |  |
Arc Profile
For curved profiles, the orientation is constrained by the profile type:
Working type | Vertical Orientation | Horizontal Orientation |
Concave | 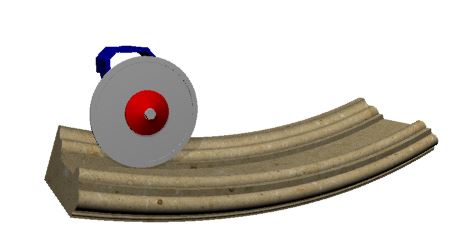 | 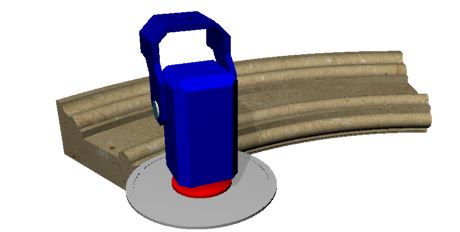 |
Convex | 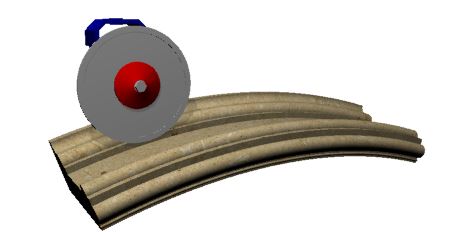 | 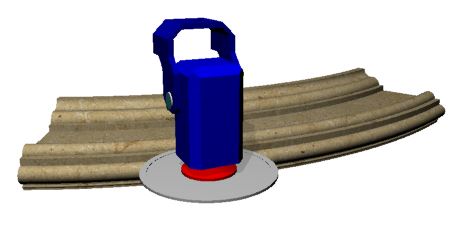 |
Working type
The working can be performed in two modes:
 | Cut mode |
 | Sweeping mode |
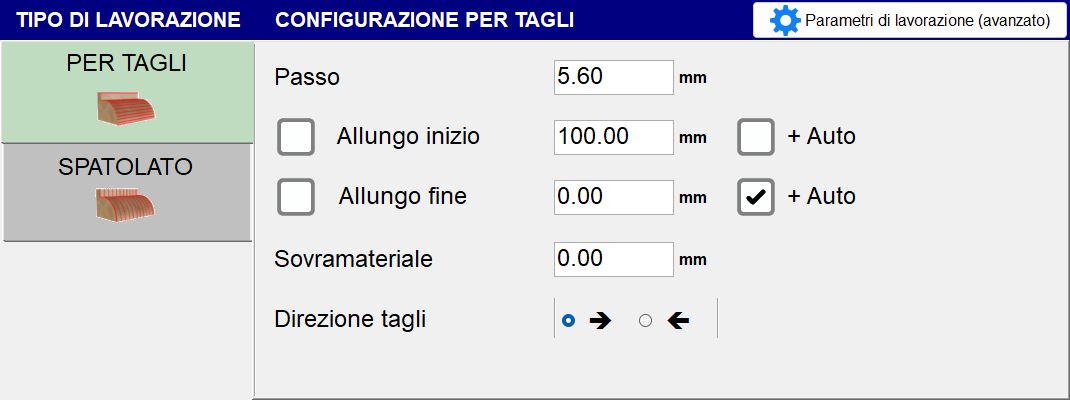
Cut Configuration
Parallel cuts following the selected profile are performed at a distance between cuts taken from the parameter.
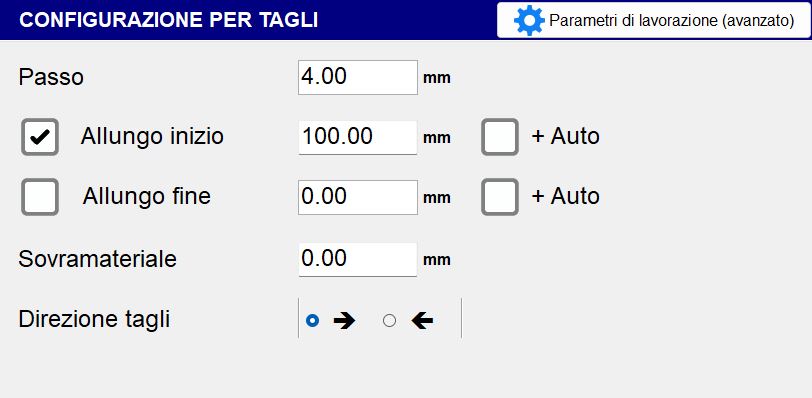
Step | Indicates the distance between the position of one cut and the adjacent cut. If it is greater than the disk thickness, material remains between passes. |
Start / end extension | Allows a cut to be extended at the start / end by the set value. |
Auto Plus | Enabling the flag automatically increases the extension value based on a value established by the system. |
Offset work | Thickness of material to be left above the desired final section. |
Cut direction | The cut can run from right to left or from left to right, depending on the selected configuration. |
Sweeping Configuration
The movement is transverse to the profile direction and is used for surface finishing of the piece.
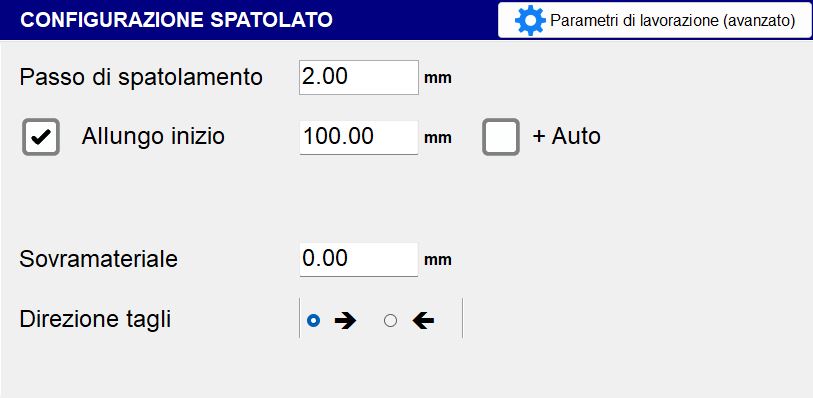
Sweeping step | Indicates the distance between one transverse movement and the next along the profile direction. |
|---|
Cutting speed and mode
Depending on the previous selections, different menus appear for selecting the parameters required to define the working.
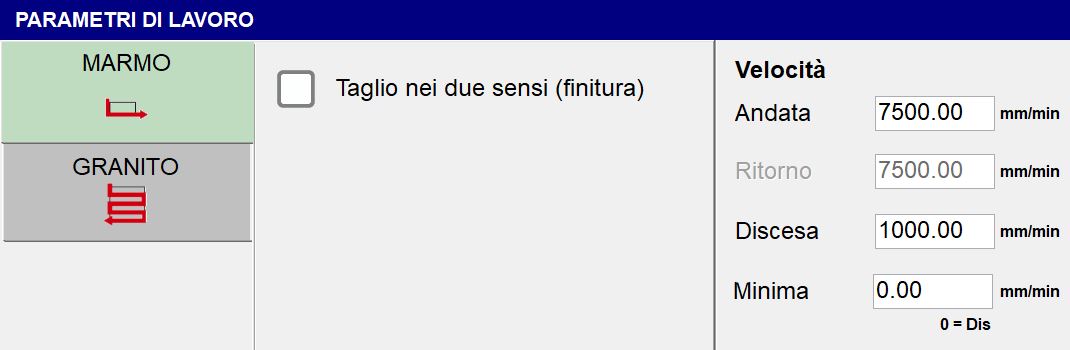
If the selected working type is Cut Configuration, two types of working parameters are available:
 | Marble Mode |
 | Granite Mode |
Marble Mode
General parameters:
Cuts in both directions (finishing) | This flag allows a return speed different from the forward speed to be set. |
Never lift (finishing) |
Speed parameters:
Forward | Forward execution speed of the pass. |
Return | Return execution speed of the pass. |
Penetration | Penetration execution speed of the pass. |
Minimum | When a value other than zero is set, the cutting speed depends on the depth of the cut itself. The movement therefore uses the forward speed for cuts at zero depth and the minimum speed when the cut is at the maximum depth for the selected section. |
Granite Mode
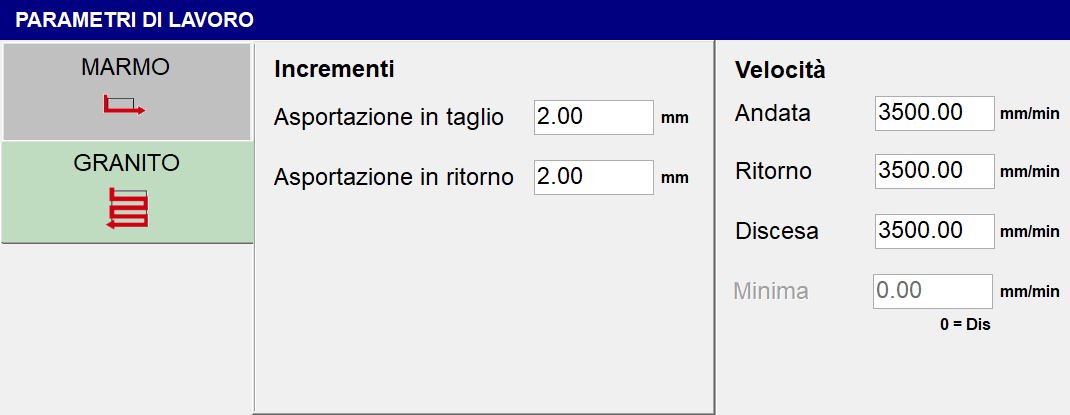
General parameters:
Material removal during forward cut | Amount of material removed during the forward pass. |
Material removal during return | Amount of material removed during the return pass. |
If the selected working type is Sweeping Configuration, only one working parameter is available:
Speed - Working | Sets the speed at which the sweeping working type is performed. |
|---|
Working parameters (advanced)
 | Working parameters (advanced) |
This screen can be used to check and edit various parameters, many of which were set in steps 2 and 3.
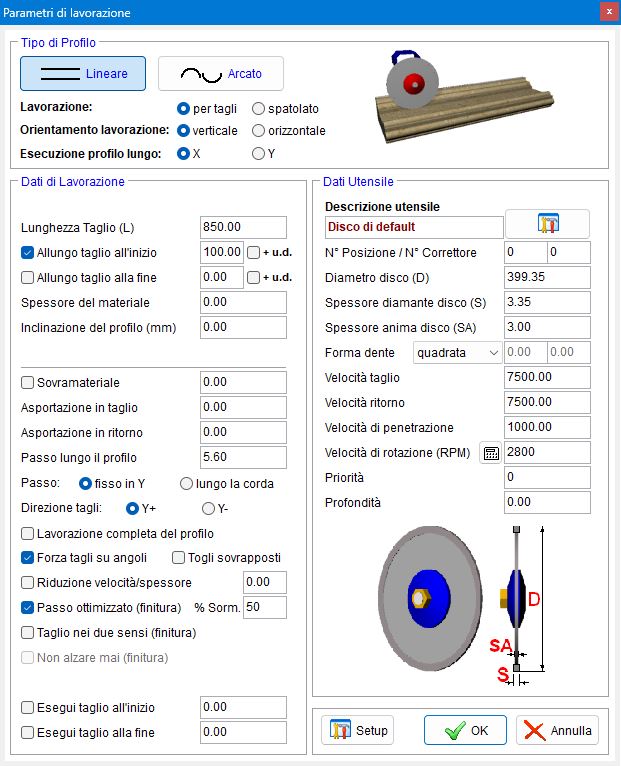
The first operation consists of selecting the profile type to be used:
 | Linear |
 | Arc |
Then the following parameters:
Working | Can be cuts or sweeping. |
Working orientation | The working can be performed vertically or horizontally. |
Execute profile along | Along X or Y. |
Working Data
The following parameters can be set for the Linear profile:
Material thickness | Defines the material thickness (in mm) |
Profile inclination (mm) | Defines the profile inclination by specifying the height difference between the end point and the start point. |
For the Arc profile, the parameters set in the previous steps are available.
Both profiles also share the following working data:
Step | Fixed in Y: keeps the distance between cuts fixed regardless of the underlying section |
Cut direction | Choice between “Y_” or “Y-”. |
Complete profile working | Allows you to choose whether or not to machine the complete profile. |
Force cuts at corners | Adds cuts at points where the slope changes. |
Remove overlaps | If this flag is enabled and the “Step” value is greater than the “Thickness” value, overlapping cuts are removed. |
Optimised step (tinting) % Overlap | If the “Step” value is lower than the “Thickness” value, the step is optimised on horizontal lines. |
Perform cut at start | Allows you to choose whether or not to perform a cut at the start of the profile. The depth of this cut can be set in the adjacent box. |
Perform cut at end | Allows you to choose whether or not to perform a cut at the end of the profile. The depth of this cut can be set in the adjacent box. |
Tool Data
Some previously set data and other tool-specific parameters are shown here.
Tool description | A brief description of the tool |
 | Tool magazine |
Position No. | Indicates the position number of the selected tool within the magazine. |
Corrector No. | Indicates the number that identifies the name of the selected tool. |
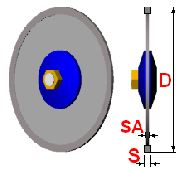
Disk core thickness (SA) | Thickness of the central load-bearing body of the disk. |
Tooth shape | The operator can choose one of three tooth shapes:
|
 | Material selection
|
Priority | A priority value can be set (strictly positive). |
Depth | Indicates the tool cutting depth. |
Working (step 4 of 4)
Based on the previous selections, a preview of the calculated cuts is displayed. The page is divided into several areas containing commands for managing changes.
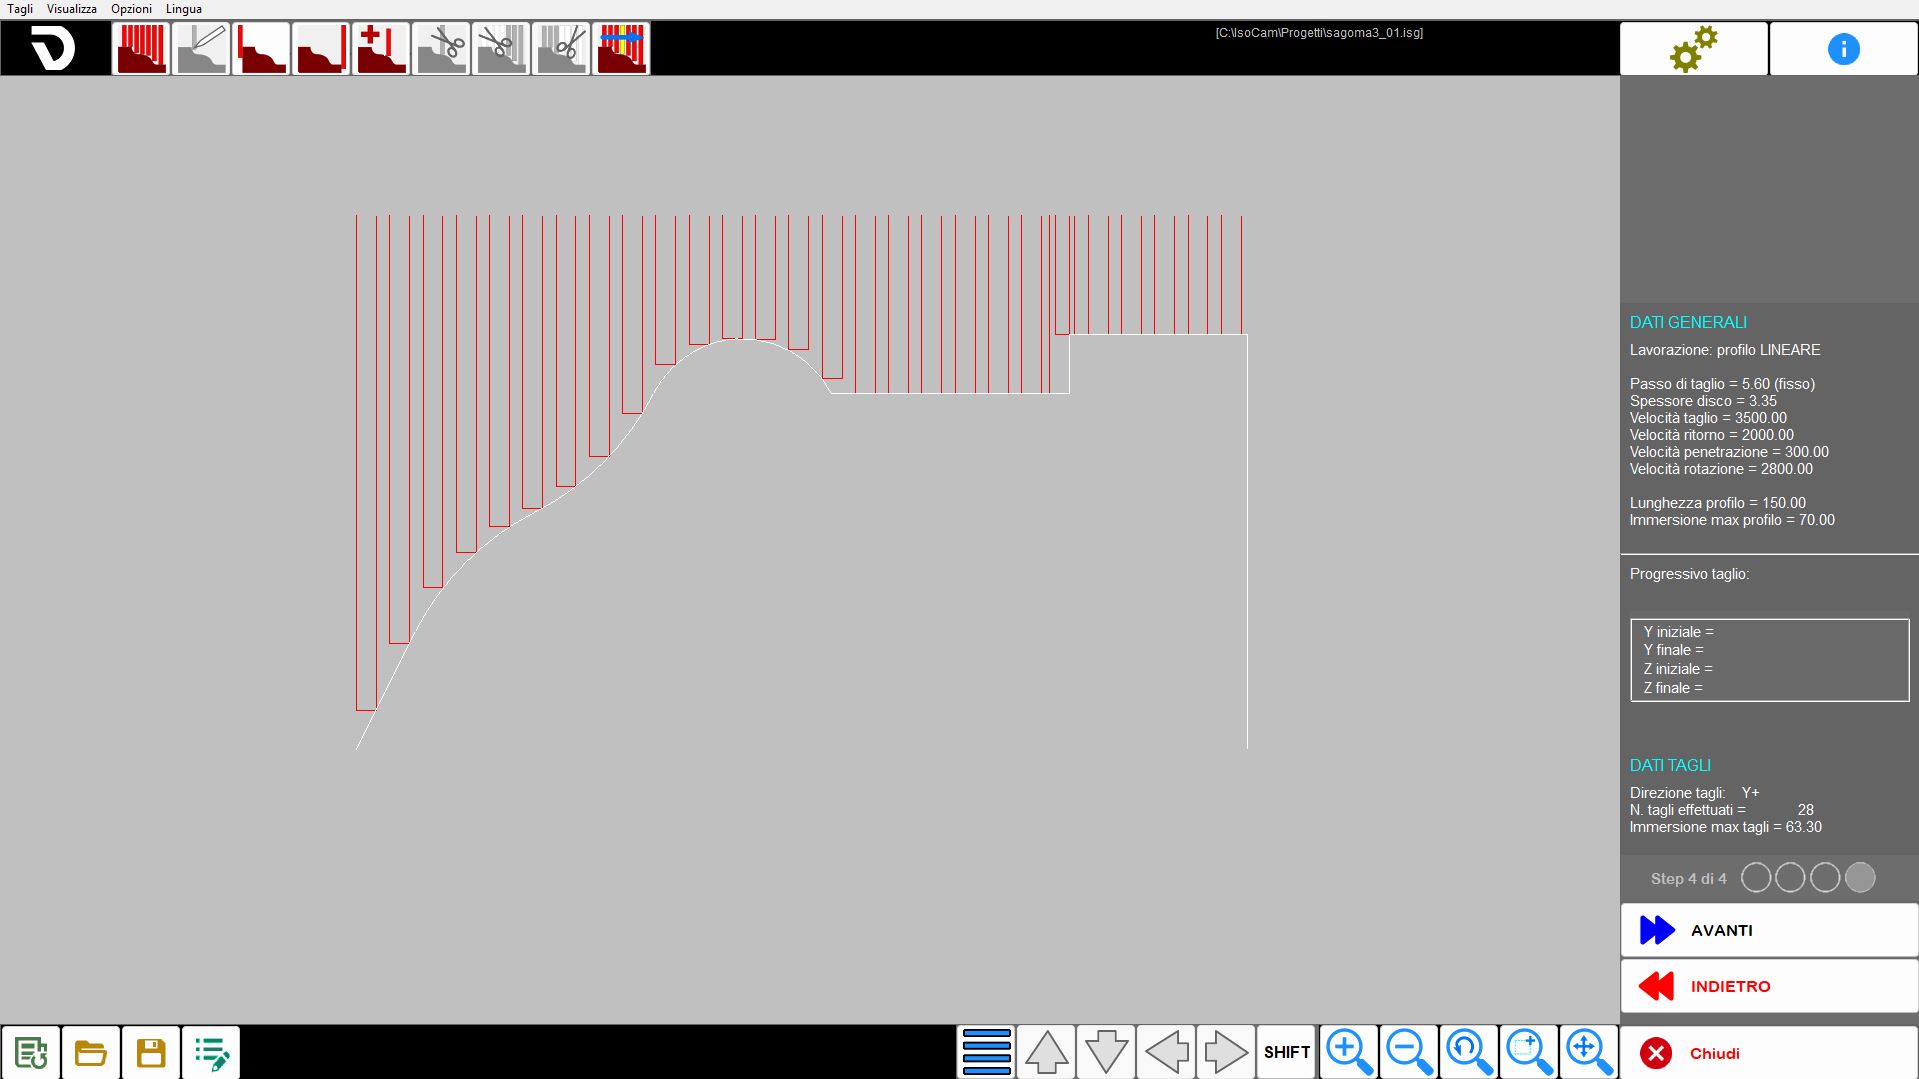
After checking the cuts or making the desired changes, press the “NEXT” button to open the page used to generate the cutting program.
Menu
In the fourth step, an additional item becomes visible in the top menu:
Cuts | This menu provides the operator with several quick settings for the generated cuts. |
|---|
Top bar
 | Cut generation |
 | Change cut position |
 | Add head cut for piece separation |
 | Add tail cut for piece separation |
 | Add a cut at the mouse position (Ins) |
 | Delete selected cut |
 | Delete cuts before the selected cut |
 | Delete cuts after the selected cut |
 | Cut simulation |
Central area
Right sidebar
In the fourth step, this bar contains the following information:
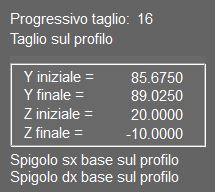 | Sequential cut number |
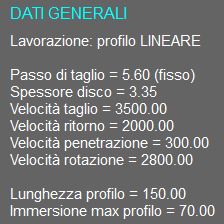 | General Data |
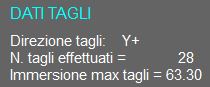 | Cut Data |
Bottom bar
 | Cut options |
  | Move/extend cuts |
 | Shift |
Program creation
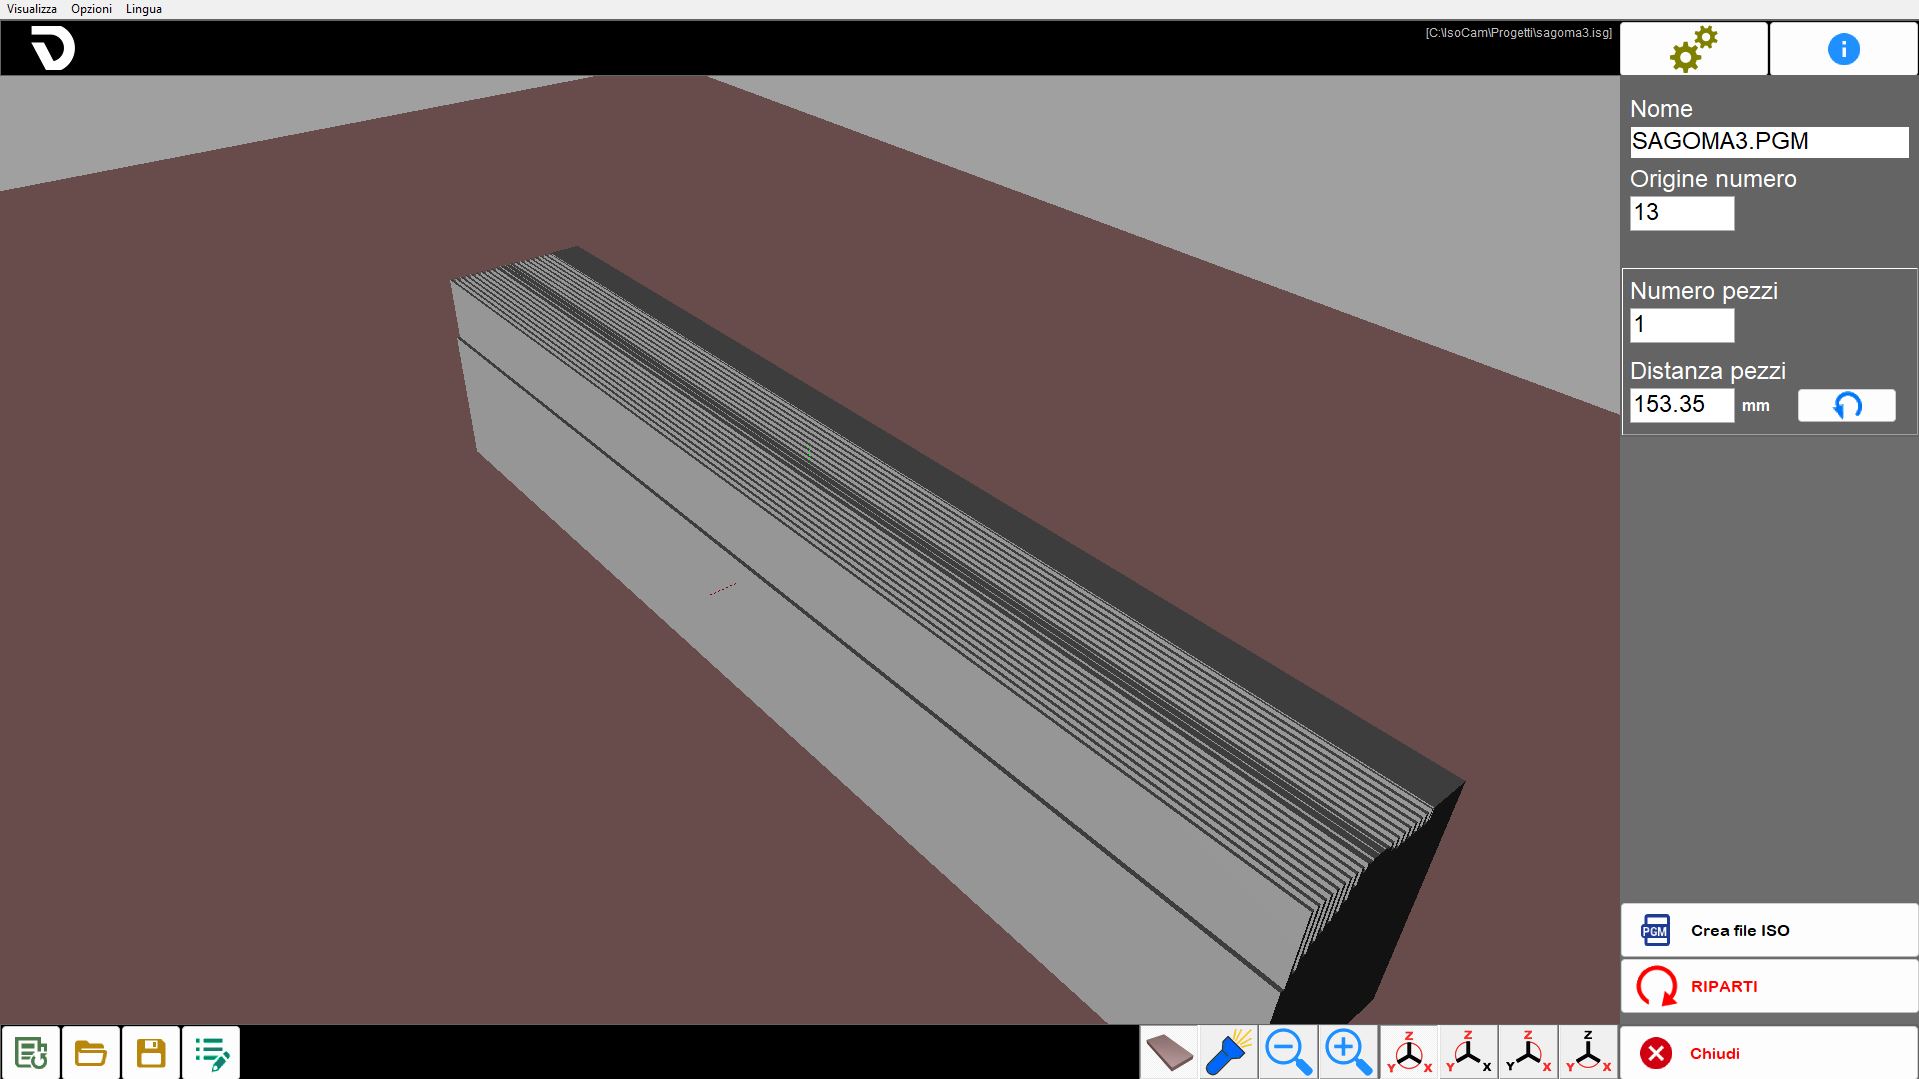
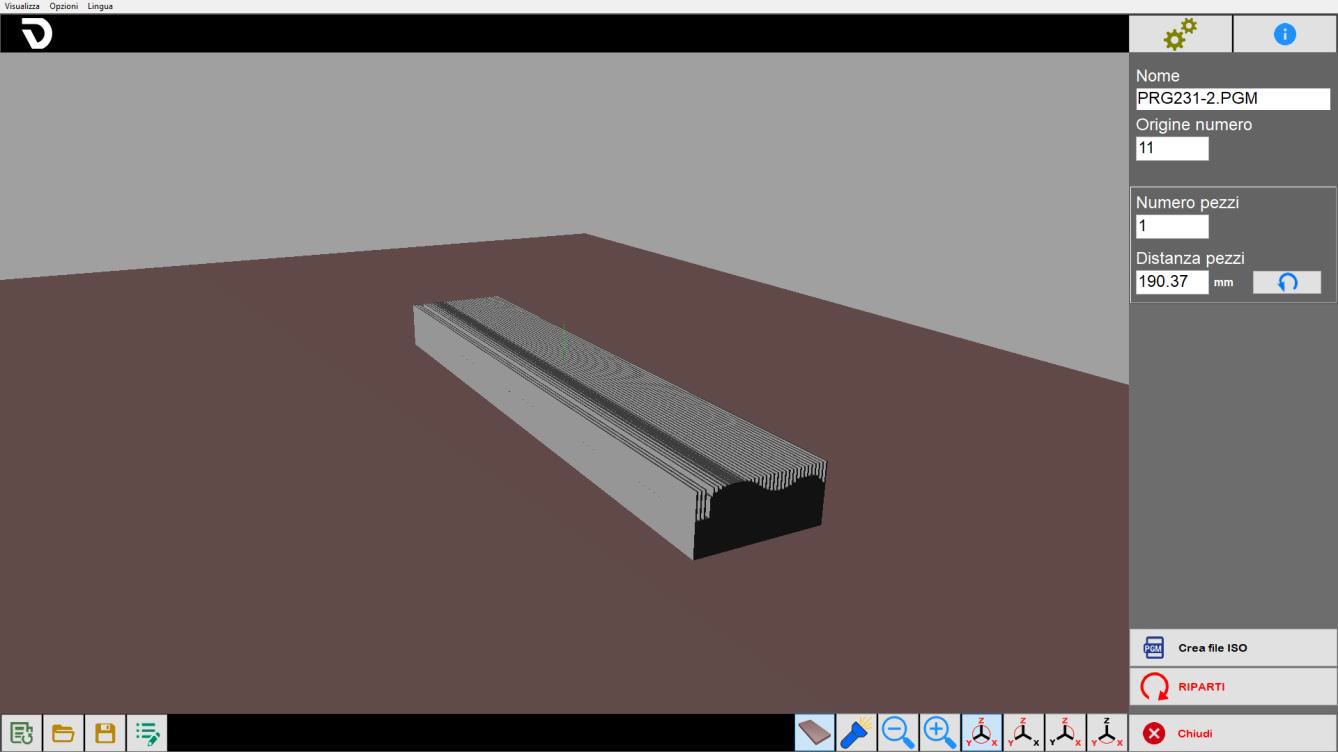
Once preparation in the fourth step is complete, the final stage can be accessed, which includes displaying the result obtained and generating the ISO file.
The 3D view of the generated working is shown in the central area, taking the working mode into account. Clicking in the area allows the view to be rotated and the zoom to be controlled.
Basic procedure
Step 1
To begin, press the “New working” button. Make sure the “Connected Segments” function is active, then enable the “line” command. Click repeatedly in the work area to draw the desired section. Once the drawing is complete, click the “line” command again to disable it. At this point, select each entity individually to check and, if necessary, edit its parameters.
Step 2
In this step, the operator can set some basic general settings relating to the required working type.
Step 3
At this point, parameters relating to the tool, type, orientation and parameters of the selected working can be set.
The “Working parameters (advanced)” panel also provides an overview of all parameters set up to this point.
Step 4
A list of cuts for the current working is generated automatically. Cuts can be inserted, edited and removed according to operating requirements.
ISO generation
The final working step allows the operator to create an ISO file from the resulting working or restart the procedure.
